


| Quantity: | |
|---|---|
The bearing base, typically made of 08MnCuNiV cast steel due to its excellent impact resistance and corrosion resistance—making it particularly suitable for marine environments—is the core load-bearing component of the white metal bearing system. It is primarily used to install and support the white metal bearing bushings, and stably transmit the loads generated by the shaft system during operation to the equipment foundation or base structure.
The core function of our Marine Upper Bearing Cover is to form a closed protective cavity for the white metal bearing system, providing rigid structural constraints for internal bearing bushes, thrust pads, and other core components. It effectively restricts the radial and axial displacement of bearing components during high-speed operation, ensures uniform load transmission to the bearing seat and foundation structure, and avoids partial load and impact damage to precision components under variable load conditions.
Our Casting Steel Bearing Cover features excellent structural strength, impact resistance, and vibration damping performance, adapting to the harsh marine environment with high humidity, high salt spray, and long-term alternating load impact. It maintains excellent fitting accuracy with the lower bearing shell after precision machining, effectively preventing lubricating oil leakage and external pollutant intrusion, significantly reducing the failure rate of the bearing system and extending the service life of the entire rotating equipment.
Parameter | Standard Specification |
Core Material | 08MnCuNiV / Custom Forged Steel |
Maximum Single Piece Casting Weight | Up to 5000kg |
Dimensional Tolerance | IT7 – IT8 Grade |
Machining Flatness | ≤ 0.02mm/m |
Bolt Hole Position Accuracy | ± 0.015mm |
Surface Finish | Anti-Rust Coating / Customized Treatment |
Key Inspection Items | PT Penetration Testing, Flatness Test, Dimensional Verification, Fit Clearance Check |
Compliance Standard | Global Marine & Heavy Industrial Equipment Standards |
Our Upper Bearing Cover for Marine Propulsion System is widely used in thrust and radial bearing systems of various marine propulsion equipment, adapting to all types of vessels including container ships, bulk carriers, oil tankers, passenger cruise ships, offshore engineering ships, fishing vessels, and coastal defense patrol ships. Beyond the marine industry, it is also fully compatible with heavy industrial rotating equipment such as hydraulic turbines, steam turbines, large compressors, power generation equipment, and metallurgical machinery, meeting the high-reliability requirements of different industrial scenarios.

The manufacturing of the 08MnCuNiV Upper Bearing Cover for marine systems begins with rigorous material selection. We specifically source premium-grade cast steel or forged steel blanks as the foundational raw material. This strategic choice of material is critical for heavy-duty industrial and marine applications, as it delivers exceptional structural toughness, superior impact resistance, and highly reliable anti-fatigue performance. By starting with top-tier steel blanks, we ensure that the marine steel bearing cover can maintain long-term stable operation even under severe high-load conditions and strong vibration environments typical of marine engineering.
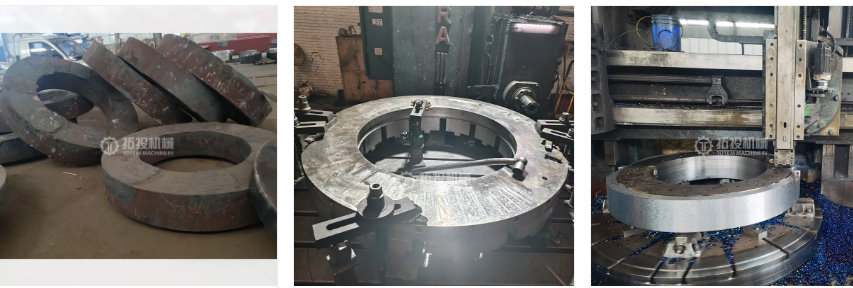
Following material preparation, the blanks undergo a comprehensive and strictly controlled precision machining process. Our advanced manufacturing facilities are equipped to handle complex geometric requirements with tight tolerances, ensuring every detail meets industrial standards. The core machining steps include:
CNC Milling: We perform precise CNC milling of the outer contour. This step is essential to achieve strict dimensional accuracy and optimal flatness requirements, ensuring that the bearing cover integrates smoothly into the overall mechanical assembly without misalignment.
High-Precision Drilling: Bolt holes are created through high-precision drilling exactly according to the client's design drawings. This meticulous attention to hole placement and sizing guarantees assembly consistency, secure fastening, and straightforward installation on site.
Deburring and Surface Finishing: To finalize the physical form, professional deburring and comprehensive surface finishing treatments are applied. Removing sharp edges and burrs is crucial to avoid stress concentration during assembly and operation, thereby significantly extending the service life of the component and enhancing operational safety.
Understanding that marine equipment and heavy machinery often require specialized configurations, we provide fully customized processing and joint design services for the 08MnCuNiV Upper Bearing Cover. Our engineering team works directly with the drawings, specifications, and technical parameters provided by clients. This flexible manufacturing approach allows us to adapt the machining process to suit different equipment structures, highly specific working conditions, and unique assembly requirements. Whether your project demands specific dimensional adjustments or specialized structural modifications, our custom machining capabilities are designed to meet your exact procurement needs.
Beyond individual component manufacturing, we pride ourselves on delivering comprehensive system-level solutions. Relying on our extensive bearing system manufacturing capabilities, we do not just supply the upper bearing cover; we can simultaneously provide a full set of supporting components for white metal thrust bearing systems. This comprehensive supply capability includes:
Thrust shafts
Thrust pads
Base rings
Balancing weights
Bearing bushes
Oil supply semi-rings
By offering a structurally complete and perfectly matched full bearing system solution, we help procurement teams and engineers streamline their supply chains. Sourcing all related components from a single, capable manufacturer ensures optimal compatibility, reduces assembly risks, and ultimately enhances the overall reliability and operational efficiency of the marine propulsion or industrial machinery system.
To ensure the highest reliability for marine applications, every 08MnCuNiV Upper Bearing Cover undergoes rigorous quality control procedures. We prioritize structural integrity and operational safety by implementing comprehensive Non-Destructive Testing (NDT) protocols prior to final approval. These stringent inspection standards are meticulously designed to guarantee that each component is entirely defect-free and fully capable of withstanding the demanding conditions of marine systems.
The visual documentation above illustrates our precise Penetration Testing (PT) execution. As a critical phase of our quality assurance workflow, this specialized testing allows our inspectors to accurately detect minute surface-breaking flaws—such as hairline cracks or porosity—that might otherwise compromise the bearing cover's performance under heavy mechanical loads. By strictly adhering to these advanced inspection methodologies, we provide procurement teams and engineers with the confidence that our marine heavy components meet exact project specifications, effectively reduce purchasing risks, and deliver long-lasting stability in critical environments.

PT
To ensure the 08MnCuNiV Upper Bearing Cover reaches your facility in perfect condition, we implement a rigorous, industrial-grade packaging protocol. Marine systems require heavy-duty castings that must be safeguarded against physical impact, moisture, and environmental elements during transit. Our packaging solutions are specifically designed to withstand the demanding conditions of long-distance sea freight and overland logistics.
Every shipment is meticulously documented and inspected before dispatch. By utilizing reinforced packaging materials and strategic loading methods, we minimize purchasing risks associated with transit damage. Whether your project demands standard delivery or specialized logistics for oversized marine parts, our shipping processes are tailored to support reliable, on-time project execution for shipyards worldwide.


