
Please Choose Your Language


| Quantity: | |
|---|---|
Within the core power transmission chains of heavy industry—spanning megaton-class centrifugal compressors to megawatt-class steam turbines—rotor systems operate at extreme linear velocities. Ensuring absolute operational stability, minimizing frictional power loss, and extending the service life of these massive rotating machines under severe conditions is a critical engineering challenge. White metal Babbitt alloy tilting pad bearings serve as the pivotal mechanical component in addressing these high-stakes demands. By integrating a highly responsive hydrodynamic structural design with premium composite material properties, they deliver a reliable rotor dynamic solution designed to protect critical industrial equipment and significantly reduce the risk of costly unplanned downtime.
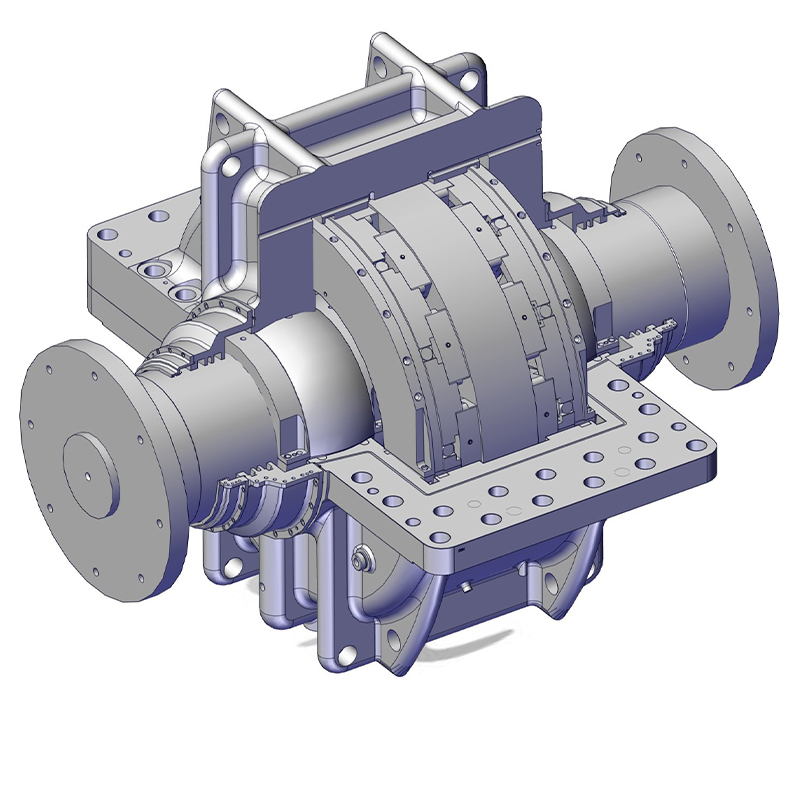
Compared to conventional fixed-pad bearings, the primary advantage of the tilting pad hydrodynamic bearing lies in its agile multi-segment structure. Engineered for dynamic adaptation, it typically consists of 3 to 5 independent arc thrust pads arranged circumferentially around the journal, providing unparalleled stability for high-speed rotors.
The Self-Aligning Mechanism: Each pad features line contact with the bearing housing via a precision-machined pivot point. When rotor speed, load, or operating temperature fluctuates, the pads freely pivot to dynamically seek the optimal attack angle. This continuous micro-adjustment generates multi-wedge hydrodynamic oil films around the journal, ensuring optimal fluid support and eliminating rotor instability.
Precision Positioning & Guidance: To prevent any axial or circumferential shifting during rigorous high-speed operation, engineers utilize a sophisticated T-slot assembly combined with locating dowel pins. This strictly defines the tilt pads' range of motion, ensuring flexible but controlled micro-adjustments within a secure envelope.
Efficient Lubrication & Heat Dissipation: Equipped with specialized inlet flow restrictors and independent oil supply channels, the lubricant is precisely distributed into the clearances of each pad. This not only guarantees stable hydrodynamic support but also significantly enhances heat dissipation efficiency, which is vital for continuous heavy-duty operation.
This advanced architecture grants the bearing inherent capabilities of self-centering and error compensation. It automatically accommodates shaft deflections of up to ≤0.3 mm and tolerates installation misalignment angles of up to 0.5°. For procurement and maintenance teams, this substantially reduces the stringent requirements for initial equipment installation, lowering setup costs and minimizing long-term maintenance overhead.
Tilting Pad Bearing
Thrust Tilting Pad
Thrust Pad Base Ring
In the manufacturing of industrial tilting pad Babbitt bearings, the composite structure of a steel backing combined with a white metal anti-friction layer is recognized as the industry standard. This precise combination effectively resolves the traditional engineering contradiction between high load capacity and wear resistance, ensuring reliable performance under extreme mechanical stress.
Robust Pad Substrate: The structural skeleton of the journal bearing pads is typically fabricated from premium 20 steel or 25 steel. This solid foundation provides exceptional structural rigidity and compressive strength, ensuring zero deformation occurs even under severe heavy-duty loads and continuous operation.
Soft White Metal (Babbitt) Working Surface: A specialized layer of Babbitt alloy—specifically the highly reliable tin-based ZSnSb11Cu6—measuring 0.8~2.5mm thick, is securely applied onto the thrust bearing pad surface. Thanks to its relatively low hardness, the Babbitt alloy exhibits excellent embeddability and conformability. If microscopic hard particles enter the bearing clearance, the white metal safely absorbs them, protecting the critical main shaft from scoring. Simultaneously, its superior lipophilicity facilitates the rapid formation of a stable hydrodynamic oil film.
High-Rigidity Bearing Housing: The outer shell of the tilting pad thrust bearing is predominantly constructed from durable ductile iron or alloy steel. Incorporating a convex spherical design further reinforces the overall support stiffness and self-aligning performance of the entire assembly, providing a secure housing for the internal components.
Thrust Pad
Tilting Thrust Pad
Thanks to the synergy of the adaptive structural design and premium composite materials, tilted pad thrust bearings exhibit top-tier mechanical attributes: high load capacity, exceptional shock resistance, and minimal power loss. They serve as a highly reliable solution in the following core industrial applications:
Centrifugal Compressors: In these critical machines, extremely high rotor linear velocities make them highly susceptible to fatal oil whip or oil film oscillation. Tilting pad Babbitt bearings fundamentally eliminate these destabilizing forces, providing peace of mind for facility operators and ensuring continuous gas compression processes.
Steam Turbines & Power Generation Sets: Whether specified for steam turbines, gas turbines, or large-scale generators, ultimate reliability is non-negotiable. The white metal pads effectively absorb vibration energy and significantly reduce frictional power loss—with measured reductions exceeding 18%—ensuring the long-term operational stability required for continuous power generation.
High-Speed Gearboxes & Heavy-Duty Pumps: Facing complex axial thrust and intense radial loads, tilting pad Babbitt thrust bearings demonstrate exceptional fatigue resistance and impact endurance. Featuring advanced Babbitt surfacing with a guaranteed bond strength of ≥55 MPa, they deliver unwavering performance in the most demanding fluid handling and power transmission environments.
The evolution of the white metal tilting pad journal bearing represents the industrial pursuit of operational smoothness and reliability. Through precise mechanical design, it transforms operational uncertainty into adaptive regulation, while its balanced composite materials resolve the deadlock between heavy loads and component wear. For modern industrial enterprises focused on maximizing efficiency, minimizing maintenance downtime, and ensuring operational stability, selecting a premium tilting pad radial bearing is an essential investment for safeguarding core power assets.
The manufacturing of White Metal (Babbitt) Tilting Pad Bearings demands a highly controlled precision engineering workflow. Because these components are critical for maintaining rotor stability under dynamic loads, every step—from initial material selection to final segmentation—must be executed with strict adherence to metallurgical and geometric tolerances. Our production process integrates advanced material treatments with precise CNC machining to ensure optimal anti-friction performance, structural integrity, and long-term operational reliability. By strictly controlling thermal dynamics and machining accuracy, we deliver bearings that meet the exacting demands of complex industrial machinery.
The foundation of a reliable bearing begins with premium raw materials. Depending on specific engineering requirements, we utilize forged annular pad blanks manufactured from high-grade 20 steel, 25 steel, or specialized alloy steel to guarantee reliable mechanical strength.
Rough Machining & Preliminary Flaw Detection: The initial phase involves the rough turning of the inner diameters, outer diameters, and end faces of the blank. Calculated allowances are carefully reserved for subsequent finish machining. Following this, preliminary flaw detection is conducted to ensure the steel substrate is completely free from internal defects such as porosity or micro-cracks, establishing a sound and reliable base for further processing.
Hydrogen Relief Annealing: To guarantee structural stability before casting, the machined blanks undergo a critical thermal treatment. The steel substrates are placed in an annealing furnace and soaked at a precisely controlled temperature of 270°C~300°C for 24 to 48 hours. This prolonged heating process effectively eliminates internal residual stresses generated during rough turning. More importantly, it thoroughly expels trace hydrogen trapped within the steel matrix. Removing this hydrogen is essential to prevent critical failures such as "blistering" or delamination of the Babbitt layer during the subsequent casting phase.
Forging Blank
Rough Machining
Achieving a strong metallurgical bond between the Babbitt white metal and the steel substrate is essential for operational safety under heavy industrial loads. The required bond strength must reach 50~80 MPa to ensure the anti-friction layer remains securely attached during continuous rotation, minimizing the risk of premature wear or catastrophic failure.
Surface Tinning (Activation): The pad blank is first subjected to rigorous acid pickling and degreasing to remove all surface impurities. It is then preheated to 250°C~300°C and treated with a specialized flux. A uniform transition layer of pure tin, approximately 0.2mm thick, is meticulously applied. This tin layer acts as a vital metallurgical bridge, significantly enhancing the adhesion strength between the steel backing and the Babbitt material.
Centrifugal Casting Process: We employ advanced centrifugal casting to apply the anti-friction layer. Molten Babbitt alloy (such as ZSnSb11Cu6) is heated to a precise temperature range of 420°C~460°C and poured into the inner bore of the rapidly rotating bearing blank. The centrifugal force drives the molten alloy tightly against the tinned inner wall, creating a highly dense, uniform Babbitt layer without internal voids. Following the pour, the cooling rate is strictly regulated—utilizing controlled water cooling or slow cooling in a holding furnace—to prevent thermal cracking and material segregation.
To guarantee strict interchangeability and precise assembly among multiple pads, we utilize an "integral machining followed by segmentation" manufacturing route. This advanced method effectively eliminates cumulative tolerance errors that frequently occur when machining individual pads separately, ensuring exact alignment and functionality.
Semi-Finish & Finish Boring: Once the Babbitt casting is complete and structurally stabilized, the internal bore of the integral bearing ring undergoes semi-finish and finish boring. This step ensures the inner diameter and roundness meet exact geometric specifications, which is critical for optimal fluid film formation and hydrodynamic lubrication.
Wire-Cut Segmentation: Following the internal boring, the solid ring is divided into individual tilting pads (typically 4 or 5 equal segments, based on the specific engineering design). We use high-precision Wire Electrical Discharge Machining (WEDM) to achieve exceptionally clean, accurate cuts without introducing mechanical stress or thermal distortion to the sensitive Babbitt layer.
Eccentric Outer Diameter & Back Arc Machining: The back of each tilting pad requires a specific eccentric arc or a precisely contoured curved surface with a pivot point. Using dedicated eccentric fixtures or square shaft fixtures for rigid positioning, the pads undergo meticulous CNC turning and grinding. This final machining phase ensures the curvature of the pad back and the pivot contact surface are absolutely accurate, allowing the pads to tilt freely and establish an optimal hydrodynamic wedge during operation.
Secure and reliable packaging is a critical factor when procuring highly sensitive rotating equipment components. For industrial white metal hydrodynamic tilting pad Babbitt bearings used in steam turbines, maintaining physical integrity and dimensional accuracy during global transit is paramount. The soft white metal alloy surfaces and stringent geometric tolerances require specialized protective packaging to prevent micro-impacts, oxidation, or deformation during complex logistics. We provide comprehensive, end-to-end shipping solutions, ranging from fundamental environmental isolation to heavy-duty transit configurations. Our goal is to ensure every component bypasses transit risks and retains its factory-calibrated precision across any shipping distance, ready for immediate deployment upon arrival.
We utilize high-toughness, anti-static polyethylene (PE) film as the primary barrier. This specialized industrial film offers exceptional puncture resistance and electrostatic dissipation. Through advanced vacuum heat-shrink technology, the film tightly conforms to the intricate contours of each individual tilting pad. This complete evacuation of air effectively isolates the bearing from ambient moisture, salt spray, and oxygen, preventing any oxidation, corrosion, or discoloration of the white metal material during extended maritime shipping or long-term warehouse storage. Additionally, multi-pad sets are individually encapsulated. We apply rust-proof Volatile Corrosion Inhibitor (VCI) paper and specialized bubble wrap cushioning to all critical contact points. This meticulous layering ensures zero metal-to-metal contact, providing maximum surface security against friction and micro-scratches.
Inner Packaging
Inner Packaging
The crate design adheres to strict full-enclosure principles to shield the contents from external hazards. The panel thickness is rigorously calculated based on the gross weight of the bearing assembly and is strictly maintained at no less than 12mm. This robust construction prevents any structural deformation during stacked storage, rough handling, or turbulent sea voyages. Inside the wooden crate, high-density polyurethane (PU) foam-in-place cushioning is strategically deployed. This expanding foam fills all interior voids, molding precisely around the bearing components to create a custom, shock-absorbing immobilization matrix that prevents shifting. Externally, the crates are heavily reinforced with galvanized steel strapping arranged in a secure grid pattern. Integrated forklift bases and reinforced skids facilitate safe, mechanized loading and unloading at ports and facilities. Clear, ISO-standard shipping marks—such as 'Center of Gravity,' 'Keep Dry,' and 'Fragile'—are prominently displayed to guide logistics personnel worldwide, ensuring proper handling at every transfer point.
Outer Packaging
Outer Packaging


